
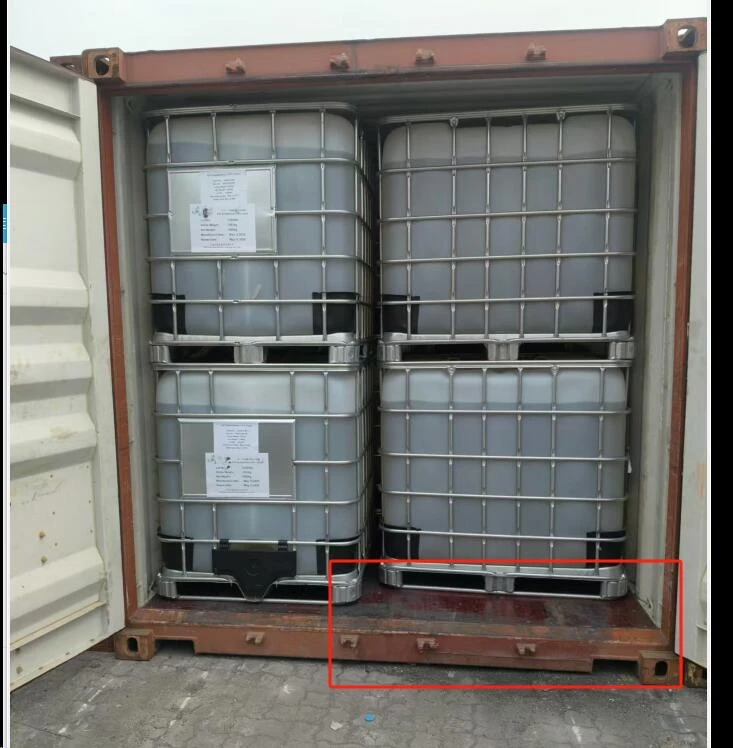
Our premium Stainless Steel Drums are engineered to provide the highest standards of containment and protection for sensitive pharmaceutical intermediates and chemical raw materials. Designed for durability and chemical resistance, these drums ensure that your high-value APIs and chemical products remain uncontaminated during storage and transit, meeting strict industry safety protocols.
Available in a comprehensive range of sizes and configurations, our steel packing solutions are optimized for versatility. From bulk bottle alternatives to specialized industrial barrels, these stainless steel containers offer superior leak-proof sealing and structural integrity, making them the ideal choice for the rigorous demands of the pharmaceutical and chemical manufacturing sectors.
Detailed Parameters
| Material Grade | High-Grade Stainless Steel | Container Type | Industrial Drum/Barrel |
|---|---|---|---|
| Available Sizes | Multiple Standard & Custom Sizes | Closure System | Hermetic Sealing Lid |
| Surface Finish | Polished/Electropolished | Compatibility | Chemical & Pharma Grade |
| Wall Thickness | Customizable based on load | Packaging Type | Bulk Industrial Packing |
| Corrosion Resistance | High-level oxidation resistance | Certification | Industry Standard Compliant |
Key Advantages
Chemical Stability
Exceptional resistance to corrosion, ensuring no reaction with pharmaceutical intermediates.
Extended Lifespan
Robust steel construction designed for long-term reuse and heavy-duty industrial cycles.
Contamination Free
Non-reactive interior surfaces prevent leaching, maintaining product purity for APIs.
Secure Sealing
Precision-engineered lids prevent leakage and protect contents from atmospheric moisture.
Versatile Sizing
A wide array of dimensions available to fit different volume requirements and storage spaces.
Standardized Fit
Compatible with standard industrial handling equipment for streamlined logistics.
Product Gallery


Management Platforms
Inventory Tracking
Real-time monitoring of drum stock levels to ensure uninterrupted production flow.
Quality Control
Strict inspection protocols for every batch to ensure weld integrity and seal quality.
Logistics Alerts
Automated notifications for shipping schedules and delivery status of bulk orders.
Compliance Audits
Digital documentation of material certifications for pharmaceutical regulatory audits.
Volume Planning
Optimized space management tools for maximizing warehouse drum storage density.
Maintenance Logs
Systematic tracking of drum cleaning and sterilization cycles for reuse.
Investment Return Comparison
| Comparison Metric | Plastic Drums | Stainless Steel Drums |
|---|---|---|
| Durability | Short-term / Single use | Long-term / Multi-cycle |
| Chemical Resistance | Limited to specific polymers | Broad spectrum pharmaceutical grade |
| Contamination Risk | Moderate (leaching possible) | Ultra-low (non-reactive) |
| Maintenance Cost | High replacement frequency | Low maintenance, high reuse |
| Environmental Impact | High plastic waste | Recyclable and sustainable |
Frequently Asked Questions
Yes, our drums are manufactured from high-grade stainless steel specifically chosen for its superior corrosion resistance, making them suitable for a wide range of aggressive chemical intermediates.
Absolutely. We provide a variety of standard sizes and offer custom fabrication to meet the specific volume and dimension requirements of your manufacturing process.
We utilize precision-engineered gaskets and heavy-duty locking rings to create a hermetic seal, preventing any atmospheric contamination or leakage of contents.
Yes, our drums are built to withstand the rigors of international shipping and comply with industrial packing standards for the safe transport of pharmaceutical active ingredients.
Due to the smooth, non-porous surface of the stainless steel, these drums can be easily sterilized using standard CIP (Clean-in-Place) methods or chemical washing.
Yes, the opaque steel walls provide 100% protection against UV radiation, which is critical for light-sensitive pharmaceutical products and intermediates.
Get a Professional Quote for Pharmaceutical Packing Solutions
Contact UsRead Our Latest News

Jul.01,2026
Boost Breeze Industrial Efficiency with NN Dimethylurea
Boost Breeze: Optimizing Industrial Efficiency with N,N-Dimethylurea In the competitive landscape of chemical manufacturing, achieving a boost breeze in production efficiency requires the use of high-purity intermediates. N,N-Dimethylurea 1,3-Dimethylurea serves as a critical building block across the textile, pharmaceutical, and resin industries. Whether it is enhancing the wrinkle-resistance of high-end fabrics or acting as a precursor for essential medicines like Caffeine and Theophylline, the quality of this chemical determines the final products performance. By leveraging professional-grade boost breeze solutions, manufacturers can ensure stability, purity, and superior results in their chemical synthesis processes.
Read More
Jun.29,2026
Industrial Use and Benefits of Pentadecanoic Acid Supplement
The Essential Guide to Pentadecanoic Acid Supplement for Industrial and Pharmaceutical Use In the evolving landscape of chemical synthesis and nutritional research, the pentadecanoic acid supplement has emerged as a critical component for specialized applications. As a saturated odd-chain fatty acid, it offers unique structural properties that distinguish it from common even-chain fatty acids. Whether utilized as a high-purity chemical intermediate in pharmaceutical manufacturing or as a specialized additive in research-grade supplements, its role in enhancing product stability and bio-efficacy is paramount. This article explores the technical specifications, industrial applications, and the strategic advantages of integrating this compound into modern manufacturing processes.
Read More
Jun.27,2026
Enhance Livestock Health with Premium Animal Supplements
Enhancing Livestock Health with Premium Animal Supplements In the modern agricultural and pharmaceutical landscape, the demand for high-efficacy animal supplements has surged as producers seek to optimize growth, immunity, and overall well-being of livestock. Among the most critical components in advanced nutritional formulations is Glycyl-L-glutamine monohydrate , a potent dipeptide that supports intestinal integrity and metabolic efficiency. By integrating pharmaceutical-grade chemical intermediates into feed additives, manufacturers can significantly reduce mortality rates and enhance the quality of animal protein. This guide explores the technical advantages of specialized amino acid derivatives and their role in the global chemical and pharmaceutical manufacturing sector.
Read More